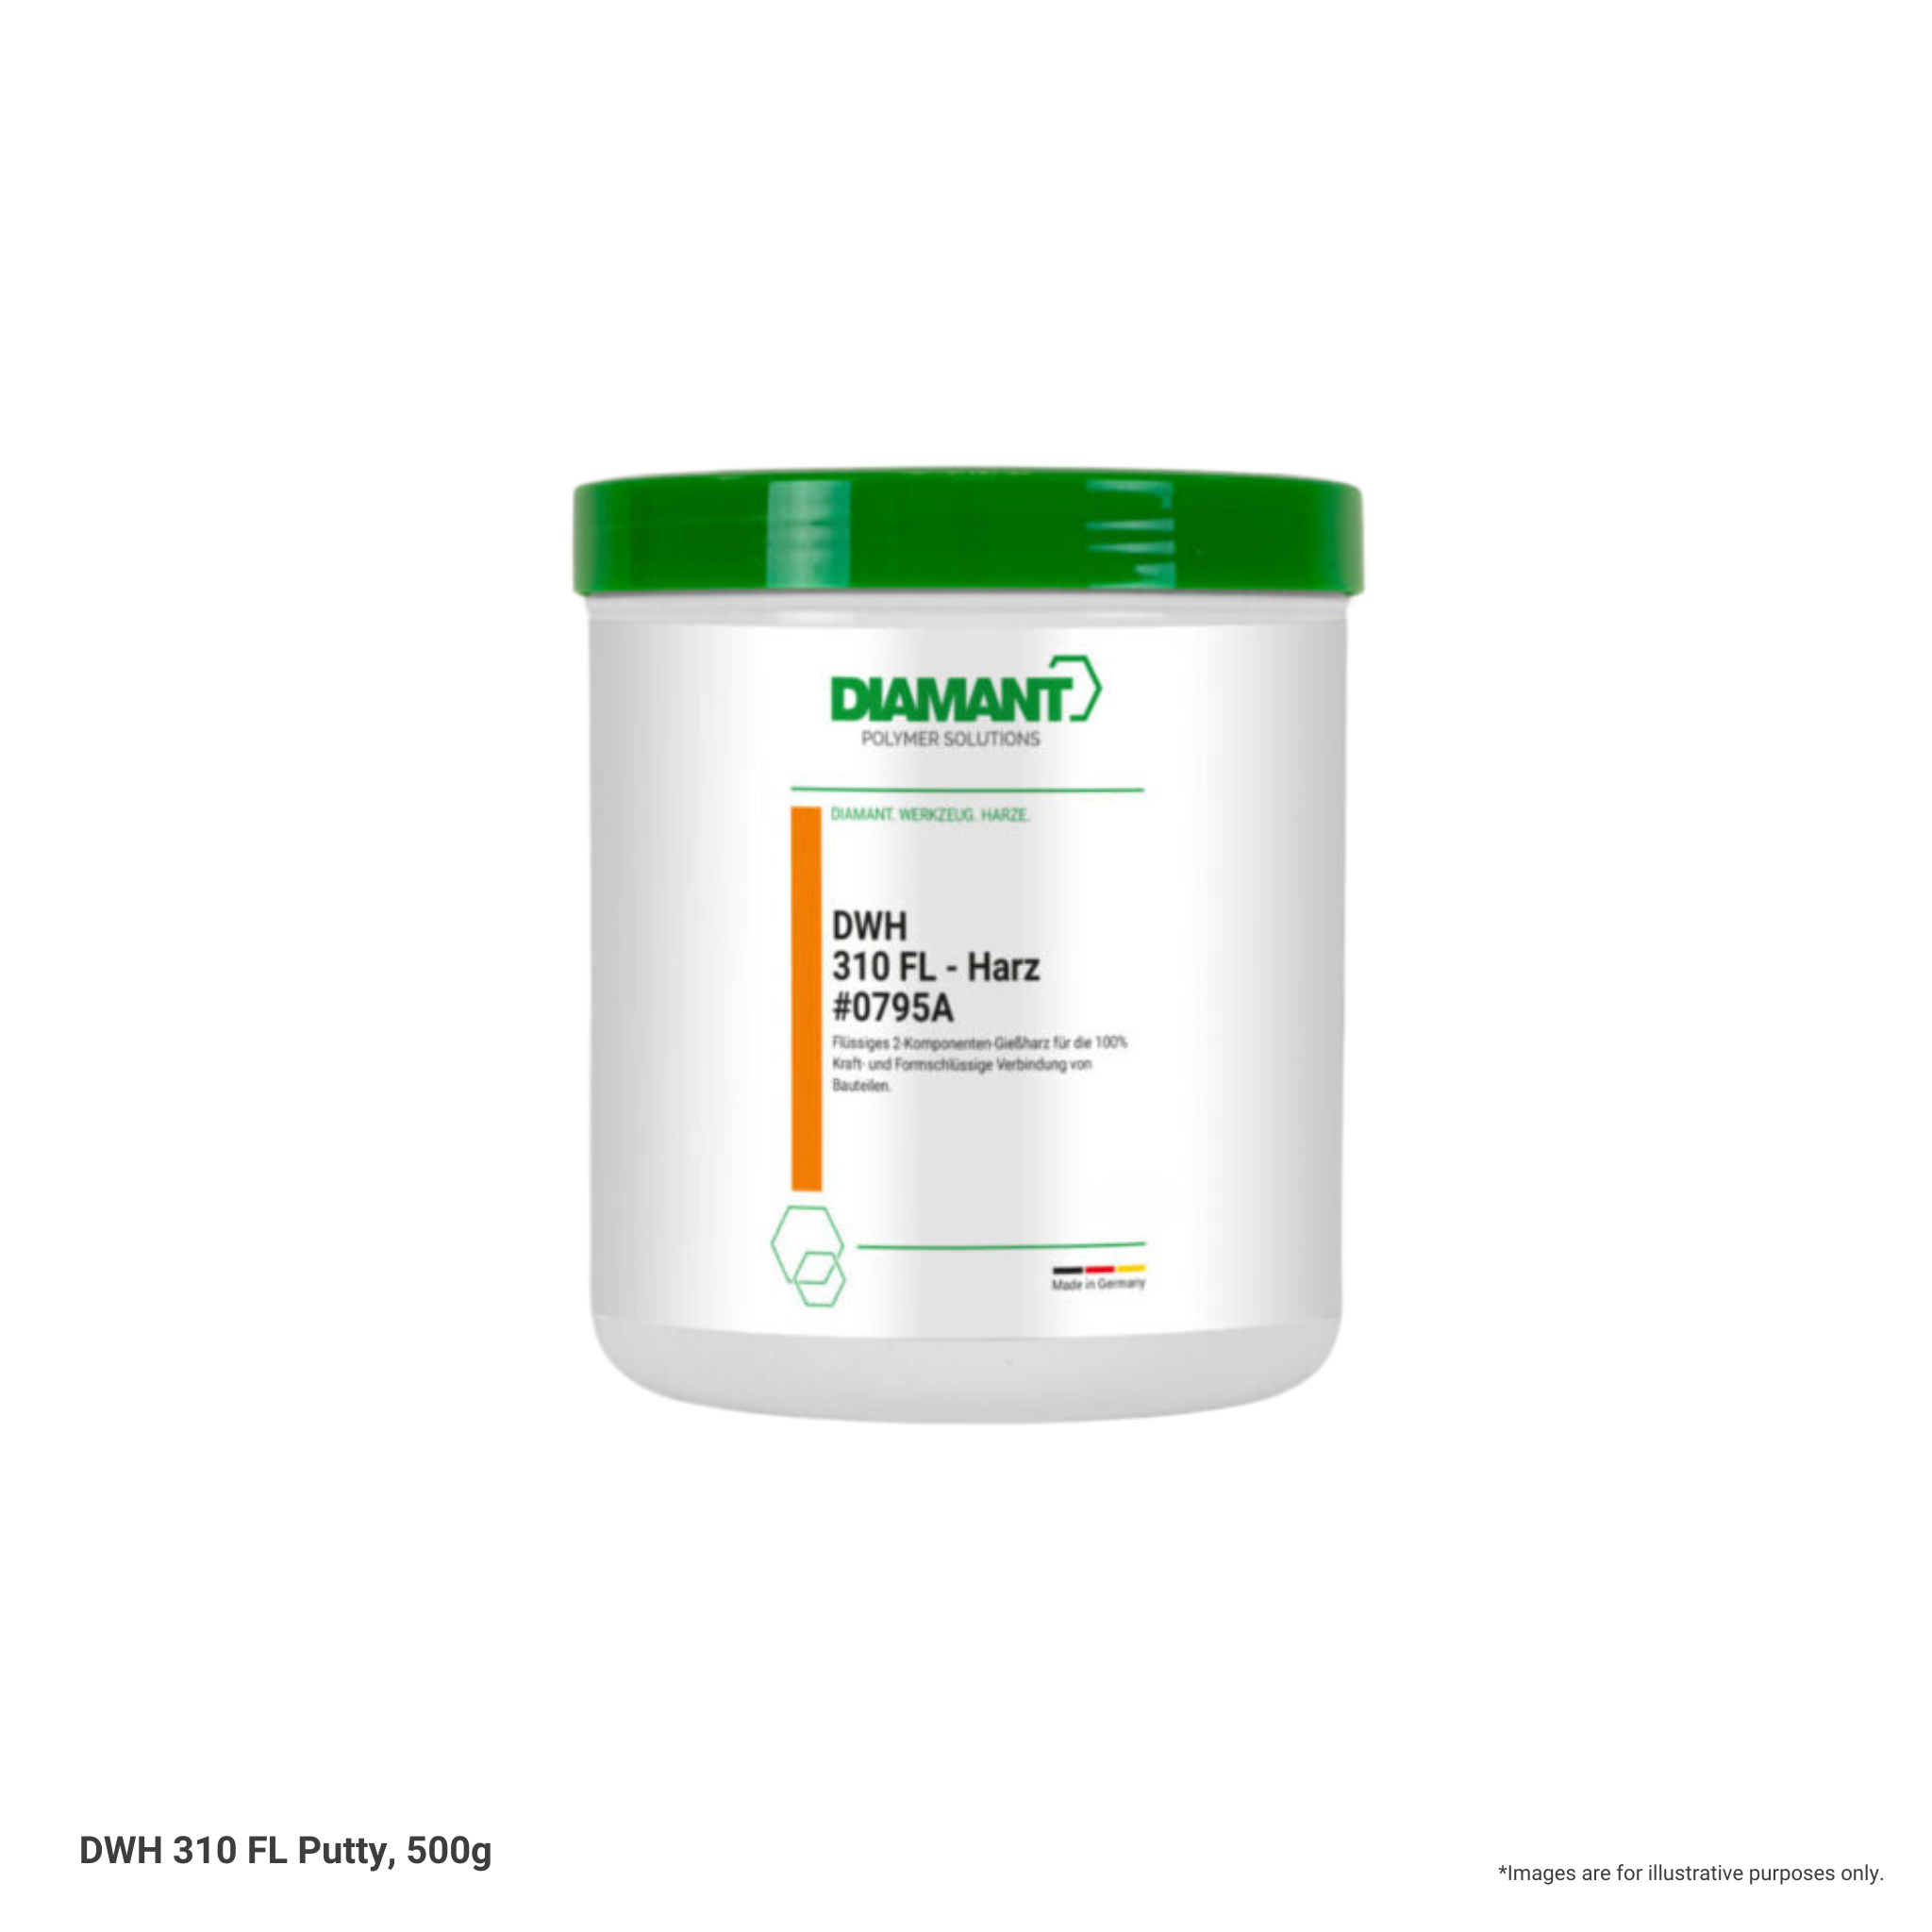
DWH 310 FL Putty, 500g
Original price was: $169.00.$50.70Current price is: $50.70.
DWH 310 FL is a low viscosity 2-component fine adjustment and adhesive coating based on epoxy resin with steel fillers. It is used for form-fit and force-fit filling and bonding of parting lines on components, assemblies and parts made of a wide variety of materials. Using casting, injection and molding, even complex shapes and structures can be created with precision in the μm range. DWH 310 FL can be removed by applying a micro-thin layer of diamond release agent to the mating surface. The result is an exact copy of the molded surface. High-precision surface preparation and mechanical reworking of the surfaces is not required. In modern production technology, process times and costs can be reduced many times over. Typical applications Positive and non-positive installation of guides in mechanical engineering Adjusting lining for assemblies and elements made of a wide range of materials. Full-surface relining of strips and elements as a replacement for lining sheets. Load-bearing gap compensation on beams of portal milling and gantry systems μm- precise casting of bushings, centering and guide elements Fixing and / or centering of bearing bushes after high-precision alignment As a filler and composite material in 3D printing + additive manufacturing Properties Very high accuracy, μm-accurate molding Very high compressive strength Extremely dimensionally stable after curing Excellent load transfer due to full contact surface contact Temperature resistant up to +80 °C Excellent damping properties due to the modulus of elasticity of approx. 8700 N/mm2 Steel-grey color after curing High resistance to oils, cooling emulsions, mineral and synthetic coolants and lubricants as well as many other chemicals Chemical resistance Storage / Shelf life Store in the original, unopened container in a dry, cool and frost-free place (+5°C to +20°C). Shelf life 2 years. Protect from direct sunlight. Higher temperatures reduce the shelf life. Preparation of the bonding surface The surfaces to be coated should be roughened considerably to improve adhesion. The roughening depth should be 0.5 mm (Rt = 500μm). The roughening can be produced, for example, using a cutter head with a high feed rate on a milling machine. Surfaces must be clean, dry and free of grease and oil. Mixing procedure To mix DWH 310 FL, add component B completely into the container of component A. Mix intensively using a drill and the DIAMANT mixing propeller (Prod. No. #0789) (max. 250 rpm for approx. 2 minutes). Remove any material adhering to the walls of the container with a spatula and add to the mixture. Mix thoroughly again. Deaerate DWH 310 FL should be poured into a clean container in a long, thin, uninterrupted stream Application description DWH 310 FL can be poured freely flowing into the sufficiently large gap open at the top. Alternatively, DWH 310 FL can be injected through an inlet channel into the prepared, sealed cavity after it has been decanted into a hand cartridge. To avoid air pockets, the cavity is filled from the lowest point.